The shale shaker gets the attention, but the screen does the work. Screens are the only consumable in the first solids-removal stage: they decide how much drilling fluid you keep, how much dilution you pay for, and how much wear reaches the desander, desilter and centrifuge behind them. Choosing screens well is one of the few cheap decisions on a rig that regularly saves more than it costs.
- What API RP 13C actually says about screen naming
- Mesh count, API number and non-blanked area — three numbers that must not be confused
- Matching screen fineness to the drilling section
- Flat vs pyramid (corrugated) screen surfaces
- Screen life and blinding in oil-based mud
- Fitting screens to existing shakers — the compatibility trap
- Spares planning for export projects, with an RFQ checklist
1. Why the screen decision matters more than it looks
A screen is a few dozen dollars. The cost of choosing the wrong one is not. Run coarse screens on a well that needs fine removal and the solids that pass through reach the desander and desilter as load, then reach the mud as abrasion: pump liners, bit nozzles and the centrifuge screw all pay for it. Run fine screens on heavy, sticky, oil-based mud and the screens blind within minutes, drilling fluid goes overboard with the cuttings, and the crew drops back to coarse — having burned both fluid and screens on the way down.
Screen selection is therefore a duty-point decision: flux (mud flow per unit screen area), solids loading and target discard wetness must fit together. The right question is never "which mesh is best" but "which fineness still passes the full circulating rate at this mud weight and viscosity, without blinding, at this G-force".
2. API RP 13C: the naming you should demand on every quotation
Older screen descriptions say "100 mesh" and stop. That number alone is nearly useless, because two "100-mesh" screens with different open areas and different cloth will separate very differently. The current standard, API Recommended Practice 13C (ISO 13501), describes each screen with two independent designations:
- API number (API to 25 microns cut point). The separation designation, from API 20 (coarsest) to API 325 (finest). This is what should drive your selection. It corresponds to a D100 cut point: the size of particle the screen passes almost completely.
- Non-blanked area (NBA). The actual open screen area in square metres or square feet, after the backing plate, rib support and any bonding take their share. Two screens with the same API number can differ in non-blanked area by a factor of more than two — and flow capacity follows the larger NBA, not the label.
- Conductance. The permeability of the screen cloth per unit thickness, in kilodarcy/millimetre (or equivalent). Higher conductance = less pressure drop across the screen = better fluid throughput at the same cut point.
A screen described only as "120 mesh, stainless" is not a specification. Ask the supplier for an RP 13C sheet: mesh count, API number (with the micron cut point), non-blanked area, conductance and cloth construction (bonded, frame type). Any serious manufacturer produces this sheet for each screen family.
| Designation | What it tells you | What it does not tell you |
|---|---|---|
| Mesh count | Threads per inch of the primary cloth | Nothing about open area or cut point |
| API number | D100 cut point of the finished screen | Nothing about flow capacity |
| Non-blanked area | Real open area available to the mud | Nothing about separation fineness |
| Conductance | Permeability per unit thickness | Nothing by itself about life or strength |
3. Match fineness to the drilling section
Screen fineness should follow the hole section, not habit. A practical progression used on most land rigs:
| Hole section | Typical API number | Rationale |
|---|---|---|
| Surface / large hole, high rate of penetration | API 20–80 | Very high solids loading; keep area open, protect the pump |
| Intermediate | API 80–140 | Balance between capture and throughput |
| Production / finish sections | API 140–230 + | Protect downhole tools, prepare mud for the desilters/centrifuge |
| Finishing runs / sensitive muds | API 230–325 | Only where the shaker duty point still passes with fine screens |
The pairing with downstream equipment matters: a desilter works best below ~25–44 µm solids load, and a decanter centrifuge is not a substitute for a missing screen stage. If the shaker cannot run as fine as the section requires at full flow, the correct answers are more screen area (more panels, pyramid surface), a second shaker, or acceptance of higher centrifuge load — in that order of cost.
4. Flat vs pyramid (corrugated) surfaces
Both start from the same cloth; the difference is geometry:
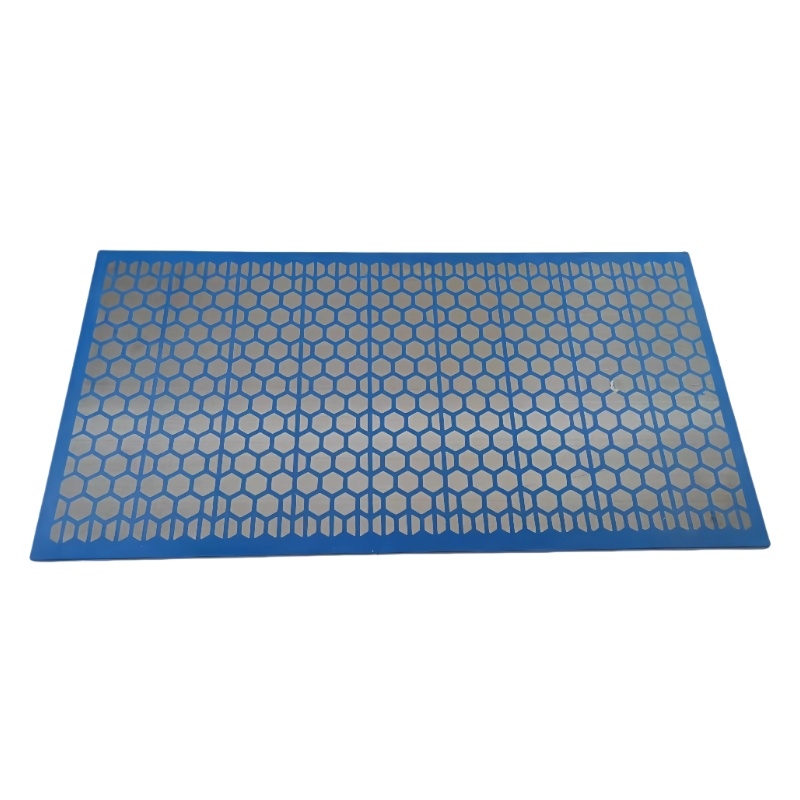
- Flat (PWP/PWL) screens: simple, cheapest, easiest to repair in the field. Lower useable area relative to panel footprint, and the cloth takes shock directly.
- Pyramid / corrugated (PMD, PWD): the cloth is wave-formed, so non-blanked area per panel increases typically by a third or more, and the ridges lift cuttings off the surface instead of letting fines plaster into the mesh. On dense, fast wells they almost always pay for the premium. For very viscous or sticky muds, large corrugations can increase near-surface turbulence in ways that either help (self-cleaning) or hurt (spray) depending on G-force — evaluate on the rig.
Three-layer bonded cloth (two support layers + separation layer) is today's norm for fine screens. It survives tensioning better than single cloth and keeps its cut point when one layer partially plugs.
5. Screen life and blinding: what actually kills screens
- Blinding (near-plugging): sticky fines bridging in openings. Common in oil-based and heavily inhibitive muds with high colloidal content. Countermeasures: step one API number coarser, raise G-force, or move the flow distribution point.
- Blinding by re-moisturised discard: too much liquid going over the end. Fix by deck angle or feed distribution, not by coarser mesh.
- abrasion at the feed: local wear where the flow lands. Rotating screens between positions spreads the wear; some crews run a sacrificial panel under the feed box.
- Corrosion and hot work near screens: never weld or grind near mounted screens; a spark burnout is invisible until the first high-solids run.
As a planning number, crews on typical land wells consume roughly 10–40 panels per well depending on section lengths, mud type and fineness — this is why spare screens belong in the original export packing list, not in a second, later shipment.
6. Compatibility: the trap in "just send screens"
Most screens sold internationally are replacements for existing shakers, and this is where quotations go wrong. Screen frames are shaker-model-specific: panel dimensions, tensioning rails, sealing bands and hook patterns must match the shaker in service. Common families include pre-tensioned frames for various linear shakers, and model-specific composite or steel frames. Screens of one brand generally do not tension correctly on another brand's deck even when panel dimensions are close.
When you request screen replacements for an existing unit, send the supplier:
- Shaker make and model, screen designation if known (e.g. the manufacturer's part number)
- Panel dimensions: length × width × frame thickness
- A photo of one screen panel from above and one at the locking edge
- API number and fineness currently in use
With those four items, a competent manufacturer confirms compatibility from its screen moulds catalogue; without them, you are buying on hope and paying for return freight.
7. Spares planning and an RFQ checklist for export projects
For a rig or project in a remote location, plan screens with the same discipline as cement and fuel:
- Commissioning set: 2–3 panels per shaker per fineness you plan to run
- Running stock: expected panels per section × number of wells before resupply, plus 20%
- Packing: export cartons with rigid separation — screens packaged loose travel badly and arrive blinded with cloth damage
- Storage: dry, away from direct sun (UV ages polyurethane and cloth bonds), stacked flat not on edge
RFQ checklist — shaker screens
- Shaker make, model and quantity of decks
- Panel dimensions and frame type (or OEM part number / one sample panel)
- Target API numbers (or hole sections and mud plan so the supplier proposes them)
- Flat or pyramid, bonded or single cloth, steel or composite frame
- Quantities: commissioning set and running stock, per fineness
- Destination port and packing standard
Lifeng Energy manufactures shale shakers and API RP 13C-designated replacement screens compatible with the common linear and balanced-elliptical shaker families, and supports project spares planning from the same drawings as the systems we deliver. Send your shaker model and planned well sections — we will return a screen proposal with API designations, non-blanked areas and packing details.
Pick shaker screens by three API RP 13C numbers — the API number (D100 cut point), non-blanked area and conductance — not by "mesh". Match the API number to the hole section (roughly API 20–80 for surface, 80–140 intermediate, 140–230+ for production runs), choose a three-layer bonded cloth and a pyramid surface where capacity is tight, and count on blinding rather than wear as the main life-killer in oil-based mud. For replacements, confirm the shaker model, panel dimensions and locking detail against the manufacturer's frame catalogue before ordering.
8. Frequently asked questions
Q: Is a higher mesh always better?
A: No. Higher mesh raises capture fineness but lowers open area and conductance. At full circulating flow, too-fine screens blind and you lose more mud than you gain in solids removal. Select the finest API number that still passes the full flow rate at your mud weight, viscosity and G-force.
Q: What is the difference between "100 mesh" and "API 100"?
A: "100 mesh" means 100 threads per inch of the primary cloth; "API 100" is an RP 13C designation meaning the finished screen passes particles up to ~100 microns at D100. Two different "100-mesh" cloths can carry different API numbers, and the same cloth in different frame types can too. Always buy and quote on the API number plus non-blanked area, never mesh alone.
Q: How many spare screens should we order with a new shaker?
A: A commissioning set of 2–3 panels per shaker per planned API number, plus a running stock sized to the expected panels-per-section times the wells before resupply, plus about 20% buffer. For remote projects, the first shipment should include the running stock — second shipments of consumables often cost more in downtime than in freight.
Q: Can we use screens from another shaker brand if the panel size looks the same?
A: Not safely. Tensioning rails, sealing bands and hook patterns are model-specific; a near-match in dimensions can still seat incorrectly and wash solids through the seal. Confirm compatibility against the manufacturer's frame catalogue using the shaker model and panel detail, or send a sample panel.
Q: Do pyramid screens really last longer?
A: The cloth life is similar; the usable non-blanked area is larger (typically a third or more) and the corrugation keeps fines from plastering the surface, so effective service time and capacity per panel are usually better on dense, fast wells. On very viscous fluids the gains depend on G-force — validate on the rig.